Oils And Fats Processing requires technologies capable of adapting the physical characteristics of raw materials to specific industrial applications. Beyond extraction and refining, fractionation plays an important role in producing oil and fat fractions with different melting and crystallization properties.
Dry fractionation allows manufacturers to separate liquid and solid fractions through controlled cooling, crystallization and filtration, without relying on solvents.
This technology is particularly relevant for palm oil processing, where the separation of olein and stearin supports the production of materials with different functional characteristics.
For industrial operators, effective dry fractionation depends on the coordination of temperature control, crystal formation and solid-liquid separation within a single processing system.
The Role of Dry Fractionation in Oils And Fats Processing
Dry fractionation is a physical separation process based on the different crystallization behaviors of triglycerides.
As an oil or fat is cooled under controlled conditions, components with higher melting points begin to crystallize, while lower-melting components remain predominantly liquid.
The resulting crystal suspension is then filtered to separate the solid and liquid fractions.
In palm oil processing, these fractions are commonly identified as:
- Palm olein: the liquid fraction, widely used in edible oil applications.
- Palm stearin: the higher-melting solid fraction, used in various food and industrial formulations.
- Palm mid fraction: a more specific fraction that can be obtained through additional fractionation stages for applications requiring particular melting characteristics.
The properties and yields of these fractions depend on feedstock composition and operating conditions.
An effective process must therefore balance separation efficiency with the required product specifications.
Controlled Crystallization and Temperature Management
Crystallization is one of the most important stages of dry fractionation.
The cooling profile influences the formation, growth and distribution of fat crystals, which subsequently affect filtration performance.
Rapid or poorly controlled cooling can produce crystal structures that are difficult to separate efficiently.
Conversely, an appropriately designed cooling program supports crystal development under more consistent conditions.
Important operating variables include:
- Initial feedstock temperature
- Cooling rate and temperature profile
- Agitation intensity
- Crystallization time
- Feedstock composition
- Target characteristics of the final fractions
These parameters must be coordinated according to the properties of the material being processed.
Technoilogy designs crystallization systems with dedicated cooling surfaces, agitators and automated control systems to support industrial dry fractionation operations.
High-Pressure Filtration in Oils And Fats Processing
Once crystallization is complete, the solid and liquid phases must be separated.
Filtration performance directly influences the quality and yield of the recovered fractions.
The characteristics of the crystal suspension, including crystal size and the proportion of solids, affect the efficiency of this operation.
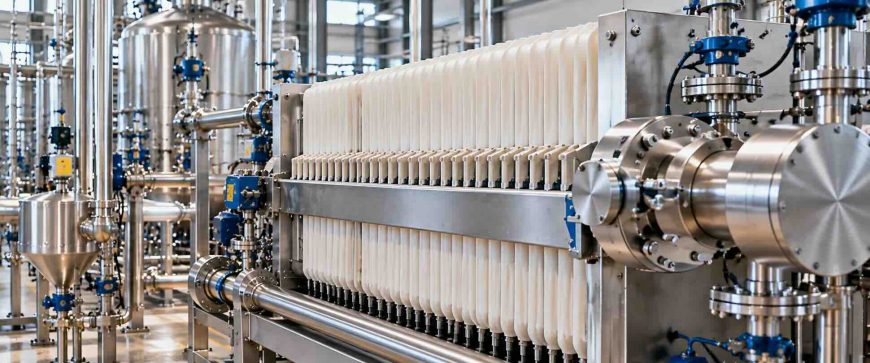
High-pressure membrane filtration is one technology used in industrial dry fractionation to separate crystallized solids from the liquid phase.
Technoilogy supplies membrane filter presses designed to operate at pressures of up to 30 bar.
The integration of crystallization and filtration is particularly important because the conditions established during cooling influence the behavior of the material during separation.
For this reason, filtration equipment should not be selected independently of the upstream crystallization system.
A coordinated engineering approach helps align both stages with production capacity and product quality requirements.
Feedstock Flexibility and Product Specifications
Industrial dry fractionation plants may process crude, semi-refined or refined oils and fats, depending on the intended application and plant configuration.
Feedstock characteristics influence the crystallization profile and the properties of the resulting fractions.
In palm oil fractionation, iodine value is one of the parameters commonly used to characterize the degree of unsaturation of the recovered products.
Different target specifications may require adjustments to cooling conditions, separation parameters or the number of fractionation stages.
Technoilogy offers dry fractionation systems designed for single or double fractionation, allowing plant configurations to be adapted to different production objectives.
The company also provides solutions for palm olein and palm mid fraction production, as well as hot filtration fractionation of stearin.
This flexibility allows manufacturers to select processing routes according to their required product characteristics.
Engineering Dry Fractionation Plants for Reliable Operation
The performance of a dry fractionation plant depends on more than the individual efficiency of its crystallizers and filters.
Material handling, cooling capacity, automation and equipment arrangement must be considered as part of an integrated production system.
Important engineering considerations include:
- Crystallizer capacity and cooling surface area
- Heat transfer and temperature control
- Agitation and crystal suspension management
- Filtration capacity and operating pressure
- Transfer of liquid and solid fractions
- Process automation and monitoring
- Cleaning, maintenance and operational accessibility
Coordinating these elements helps manufacturers establish consistent processing conditions and manage production requirements.
Technoilogy supplies dry fractionation plants across a range of industrial capacities, with configurations designed around feedstock characteristics and final product specifications.
Improving Operational Efficiency in Oils And Fats Processing
Efficient dry fractionation requires a balance between product quality, processing time and operating costs.
Cooling conditions must support the required crystal formation without creating unnecessary limitations in production capacity.
Similarly, filtration must provide effective separation while remaining compatible with the characteristics of the crystal suspension.
Automation can support more consistent operating conditions by coordinating temperature profiles, agitation and process sequences.
Energy consumption is another important consideration, particularly because cooling represents a significant utility requirement in crystallization operations.
Technoilogy develops dry fractionation systems with an emphasis on controlled operation, flexible production and low energy consumption.
By integrating crystallization, filtration and process control during the engineering phase, manufacturers can improve the coordination of the complete fractionation line.
Conclusion
Oils And Fats Processing includes specialized technologies that allow manufacturers to obtain products with different physical and functional characteristics.
Dry fractionation provides a solvent-free method for separating liquid and solid fat fractions through controlled crystallization and filtration.
The effectiveness of this technology depends on careful management of cooling conditions, crystal formation, filtration performance and plant integration.
Through its experience in industrial oils and fats technologies, Technoilogy designs dry fractionation systems that combine crystallization equipment, high-pressure filtration and automated process control.
This integrated approach supports reliable operation and the production of oil and fat fractions tailored to specific industrial requirements.